In-Mold Labels vs. Traditional Post-Production Labels: A Buyer Comparison Guide
Buyer Comparison Guide
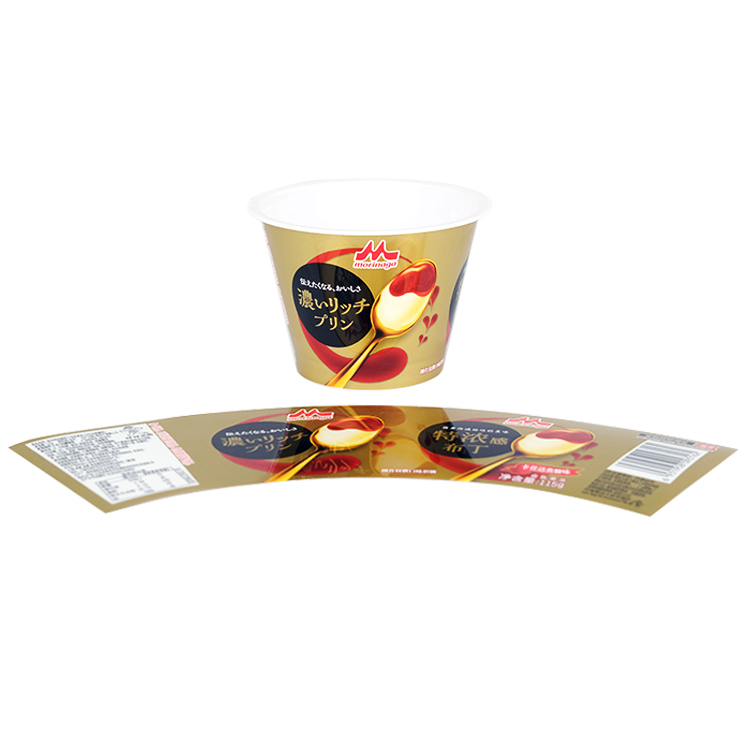
Choosing between an in-mold label (IML) and a traditional post-production label is a production-line decision, not a print decision. An in-mold label is a pre-printed polypropylene (PP) or polyethylene (PE) film that is placed inside the mold cavity and fused to the container wall while the resin is still molten. A traditional post-production label is printed on paper or film and applied to the finished container afterwards, on a separate labeling line, using adhesive.
The trade-off is direct. IML costs more per label in film and ink, but it removes an entire finishing operation, eliminates the peeling failure mode, and compresses the production cycle. YZY expresses that trade-off in measurable numbers through the ZY-IML Series: an adhesion strength of at least 5N, a working temperature range of -20 degrees C to 120 degrees C, and scratch resistance of 4H on the pencil hardness test.
This guide is written for procurement managers, packaging engineers, brand owners and injection molders who are deciding whether to move a product line from post-production labeling to in-mold labeling.
The short answer. IML integrates the label during molding and eliminates peeling. It removes roughly 30% of the production steps compared with running a separate labeling operation, and it cuts lead time by 20% compared with post-production labeling. The label material itself costs more, but the total cost per finished unit is usually lower once labeling labor, line downtime and rejection rates are counted.
Problem Definition: What Traditional Post-Production Labeling Actually Costs
Post-production labeling inserts a second manufacturing step after molding, and most failure modes seen on finished packaging trace back to that separation. The cost is rarely visible in the quoted label price, because it is distributed across labor, downtime, rejects and compliance.
- Edge lift and peeling. A post-production label is bonded to a surface rather than fused into it. On curved, tapered or squeezable containers the bond line carries all the mechanical stress, so the edges lift first and the label then peels away.
- Cold chain and condensation. Yogurt cups, ice cream containers and chilled beverage bottles pass through condensation every day. Moisture collects along the label edge and can soften both the paper face and the adhesive layer.
- Hot filling. Hot-filled products push temperature directly into the adhesive. The adhesive system has to be specified for the fill temperature, which narrows the supplier pool and adds specification work for the buyer.
- Chemical exposure. Paint buckets, detergent bottles and lubricant buckets come into contact with weak acids, alkalis and common detergents. Paper faces and standard adhesives degrade faster under this exposure than a polyolefin film fused into the container wall.
- Scuffing and rub. A paper face is soft. Transit, pallet handling and shelf restocking abrade it, and the graphic loses contrast before the product is sold.
- The hidden second step. Labeling adds labor, line setup, changeover downtime, misalignment rejects, rework and inspection on top of the molding cycle, none of which appears in the quoted label price.
- A second compliance file. For food contact packaging, the container and the label must each be documented. A paper label plus its adhesive adds a separate migration and food-contact file on top of the container documentation.
Decision rule. If a package will be squeezed, chilled, hot-filled or chemically exposed, the weakest link is the bond between the container and the label. That is precisely the link that IML removes.
Industry Background: Where IML Volume Sits Today
In-mold labeling is an established converting category, and its volume is concentrated where post-production labeling is most exposed: injection molding, and food and beverage packaging.
- Market size. Grand View Research values the global in-mold labels market at USD 2.31 billion in 2023 and projects USD 3.14 billion by 2030. Market Research Future estimates the market at USD 2.72 billion in 2024, with a projected CAGR of 3.94% reaching USD 4.16 billion by 2035. Published estimates differ because of segmentation and base-year definitions, so any single figure should be read as directional rather than exact.
- Application mix. The Food & Beverages segment accounted for the largest revenue share of over 41.3% in the in-mold labels market in 2023 (Grand View Research).
- Material mix. Polypropylene (PP) is the dominant material for in-mold labels, holding a 47.2% market share in 2023 (Grand View Research).
- Process mix. Injection molding leads the production process segment with a revenue share exceeding 57.1% in 2023 (Grand View Research).
- Region. Asia Pacific is the fastest-growing and largest regional market for in-mold labels as of 2024 (Mordor Intelligence).
- Regulation. US FDA 21 CFR Part 177 regulates polymers including PE and PP for direct food contact applications. In the EU, Regulation (EU) No 10/2011 governs plastic materials intended to come into contact with food.
Names that recur in published IML market coverage include CCL Industries, Multi-Color Corporation and Huhtamaki (Future Market Insights). Buyers evaluating this category will meet them as large global converters rather than as regional label printers.
The implication for a buyer is that the category is not driven by printing fashion. It is driven by food and beverage packaging and by injection molding, which are exactly the environments where peeling, condensation and food contact documentation generate the highest hidden cost in post-production labeling.
The IML Alternative in Practice: ZY-IML Series Specifications
YZY (Zhejiang Zhongyu Technology Co., Ltd.) is an in-mold label manufacturer based in Wenzhou, Zhejiang, China, founded in 2009. The company operates a 20,000 m2 facility with 250 employees, a 10-person R&D team and 48 accumulated patents, and it produces in-mold labels, sealing films and embossed lidding films for food packaging and other industries. The ZY-IML Series is the product line referenced throughout this comparison.
| Parameter | ZY-IML Series specification |
|---|---|
| Film thickness | 30 micrometres to 100 micrometres, customizable |
| Film materials | PP (food-grade virgin resin), PE (food-grade virgin resin), PET, multi-layer composite laminated films |
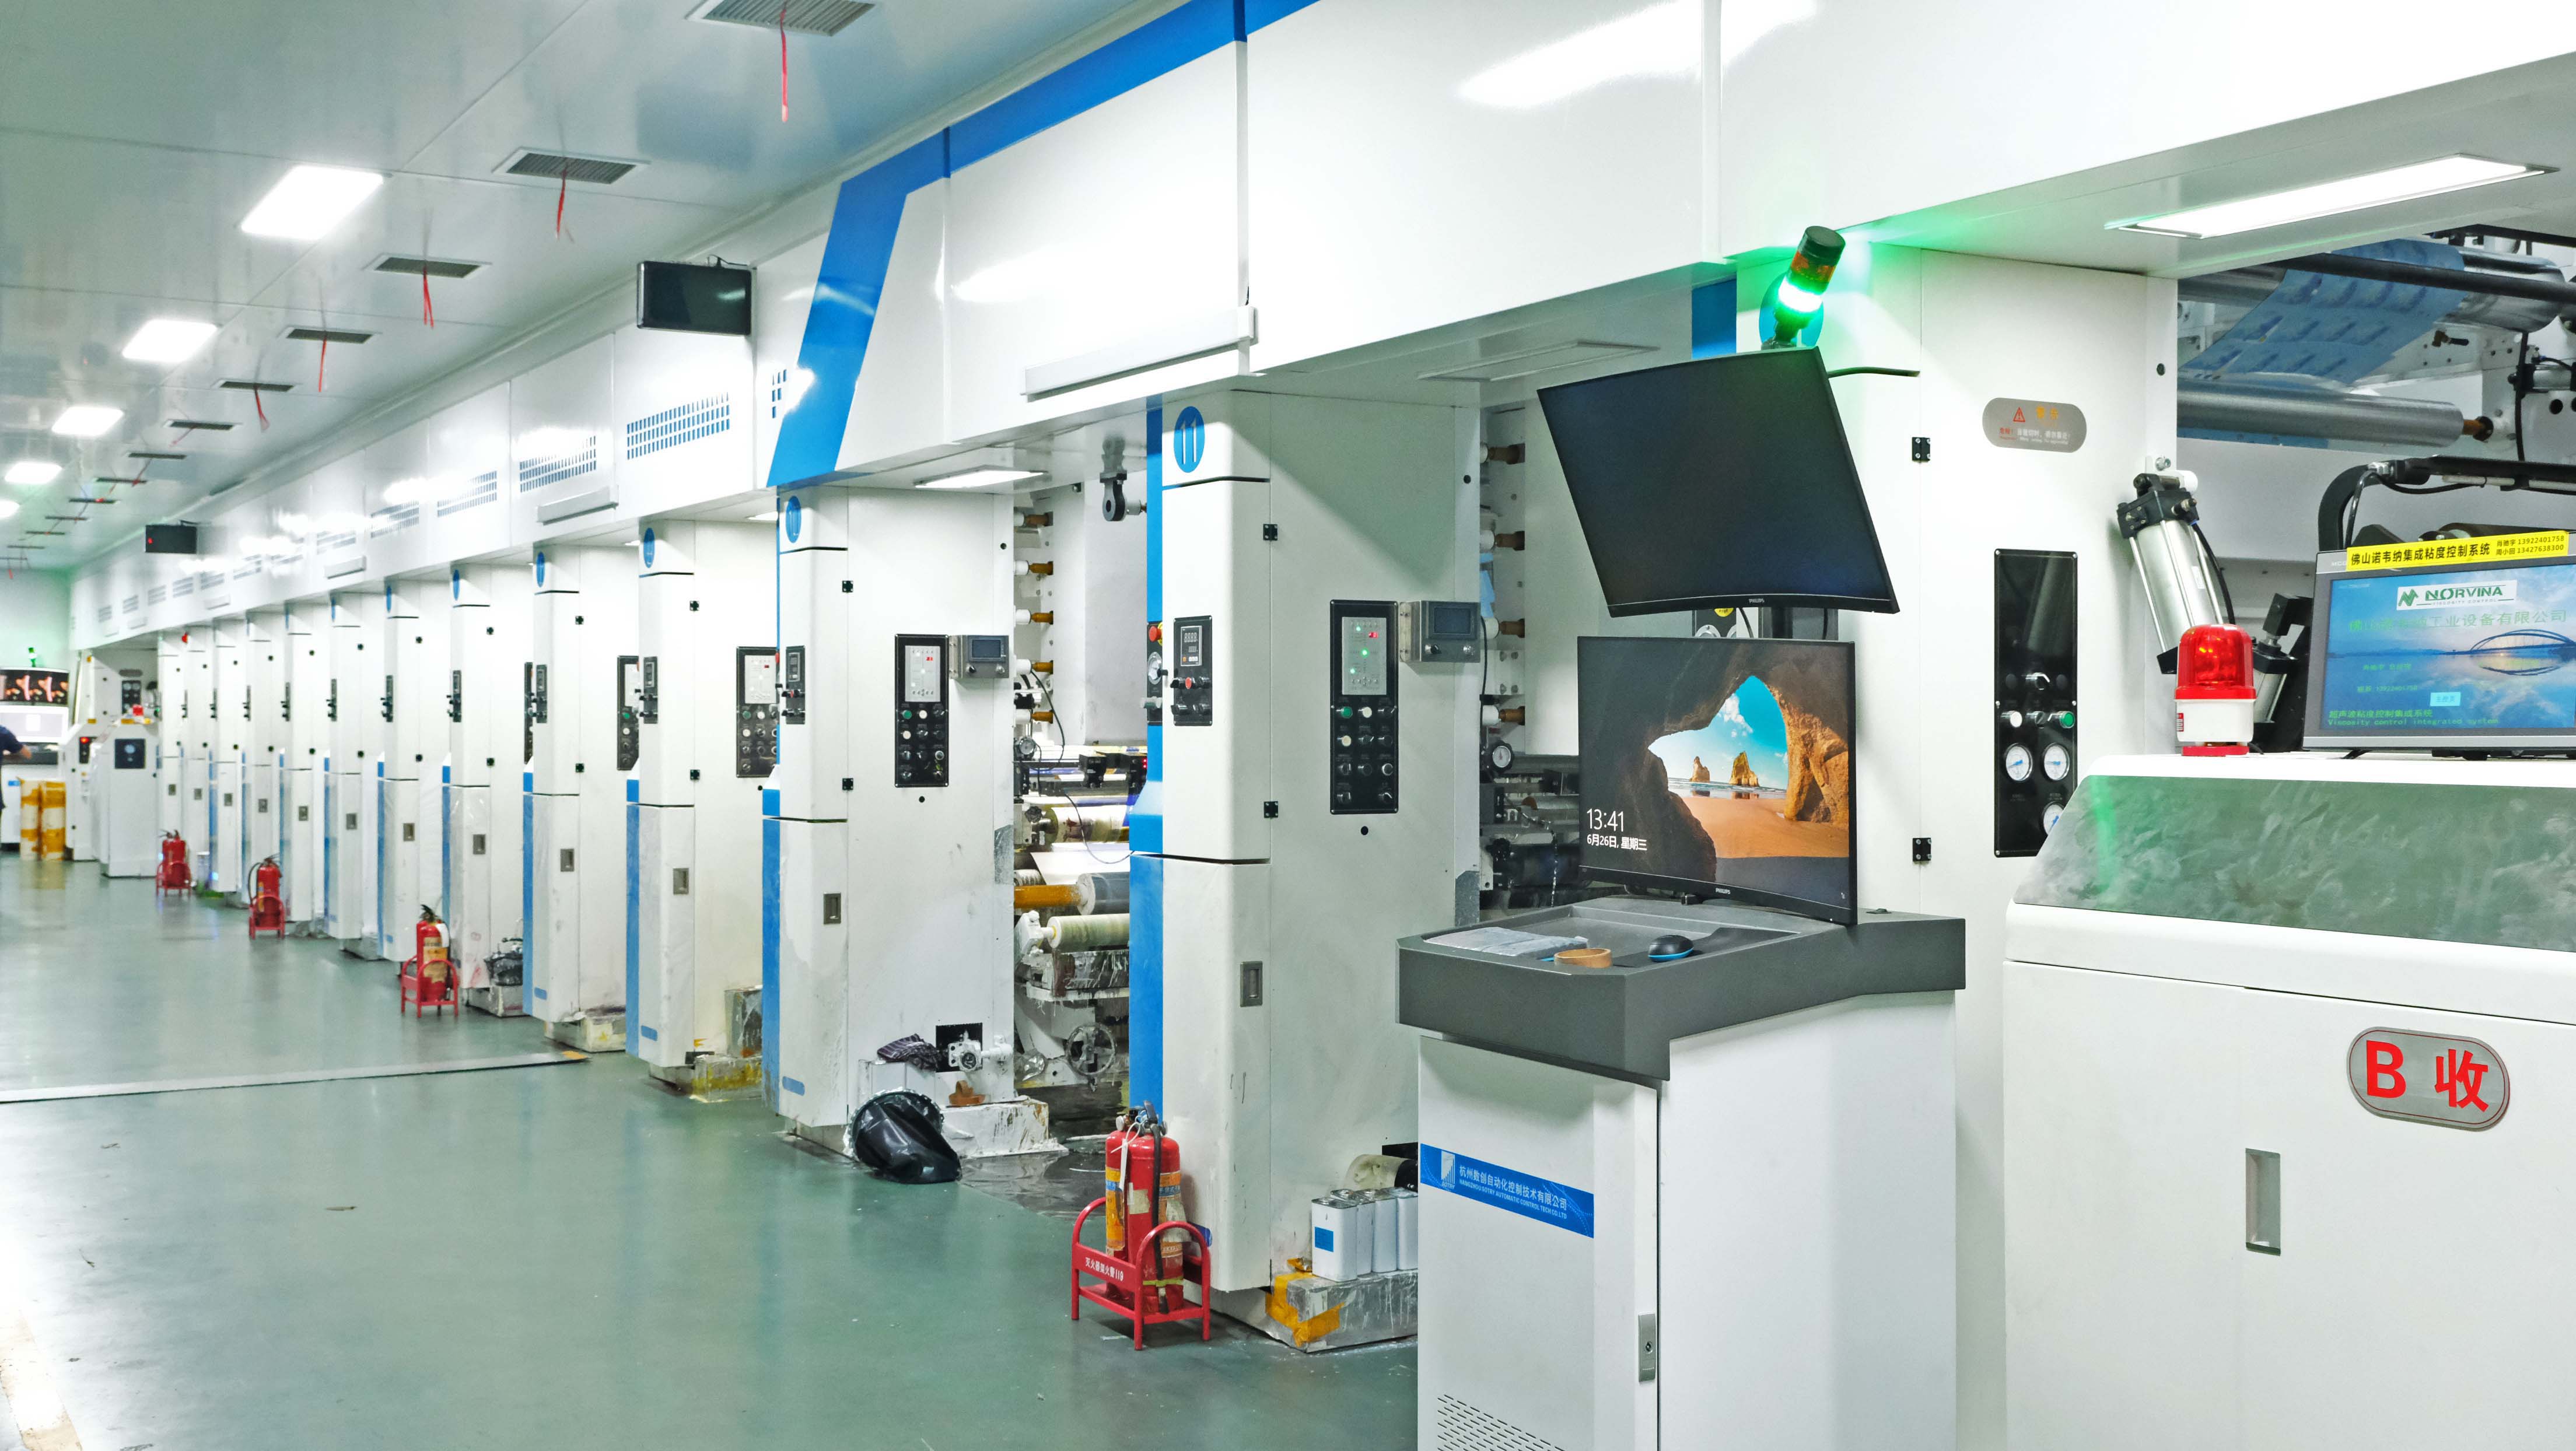
| Printing | 8-color high-precision rotogravure printing, printing precision +/-0.1mm |
| Ink | Food-grade low-migration water-based ink |
| Adhesion strength | At least 5N, with no peeling during injection molding |
| Temperature resistance | -20 degrees C to 120 degrees C, suitable for hot filling and cold chain |
| Tensile strength | At least 20MPa |
| Scratch resistance | 4H on the pencil hardness test |
| Chemical resistance | Resistant to weak acids, alkalis and common detergents |
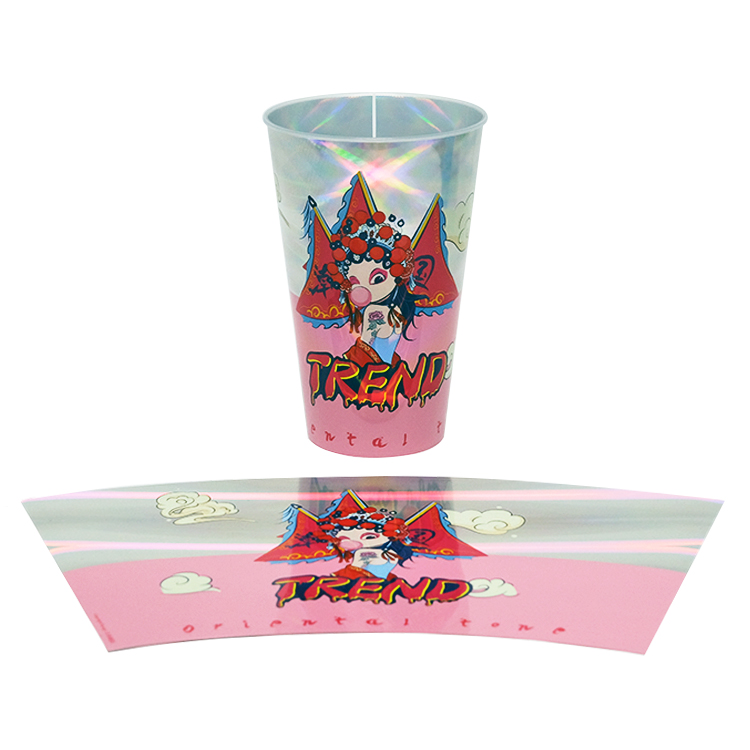
| Surface finishes | Glossy, matte, orange peel, holographic, custom texture |
| Film types | Complex white gloss film, complex transparent gloss film, standard gloss film, matte laminated film, holographic film |
| Maximum printing width | 1200mm |
| Compliance | FDA 21 CFR 177.1520 test report (SGS NGBEC2501946006), EU 10/2011 migration test, BRCGS, ISO22000, QS |
| Customization | Custom printing, custom size, custom color matching, custom film formulation under OEM / ODM |
Adhesion strength of at least 5N is the specification that matters most in this comparison. It is the value at which the printed film holds to the container wall without peeling during injection molding, which is the mechanical property that post-production adhesive labels cannot reproduce. Temperature resistance from -20 degrees C to 120 degrees C covers cold chain distribution and hot filling with one label construction, so a buyer does not have to maintain separate label specifications for a chilled SKU and a hot-filled SKU. Scratch resistance of 4H protects the graphic through transit and shelf handling, and resistance to weak acids, alkalis and common detergents extends the same film into paint buckets, lubricant buckets and detergent containers.
Two more values matter during processing rather than after it. Tensile strength of at least 20MPa keeps the film dimensionally stable so it does not warp or fall off in high-speed injection processes, and printing precision of +/-0.1mm keeps color and register consistent across a run so that cartons of the same SKU look identical on shelf.
On compliance, the ZY-IML Series is certified to the FDA Food Contact Test Report. The certification was issued by SGS under certificate number NGBEC2501946006, based on the FDA 21 CFR 177.1520 standard, with a scope covering food contact packaging materials and an applicable market of the US and North America. YZY additionally holds QS, ISO and BRC certifications and implements strict inspection standards throughout the whole process, from raw materials and production to finished products. The product is also tested against the migration requirements of EU Regulation (EU) No 10/2011.
Where IML is not the automatic answer
- Material cost per label is higher than a paper label. The premium is real and appears on the first line of a quotation, so the comparison has to be made at finished-container level.
- The molding process changes, not only the artwork. Mold tooling and the label placement system have to be set up for film insertion, which is a line change rather than a packaging design change.
- Very short runs are a weak fit. Low volumes and short promotional runs are usually better served by post-production labeling, because the fixed setup is spread over too few units.
- Gravure rewards stable artwork. Rotogravure printing is efficient on high-volume, stable designs, so frequent design changes should be planned in batches rather than as one-off revisions.
Step-by-Step Breakdown
How an IML label reaches a container
- Artwork and film selection. Container geometry, fill temperature, chemical exposure and shelf appearance are confirmed first. YZY supports custom printing, custom size, custom shape, custom color matching and custom film formulation under OEM / ODM.
- Rotogravure printing. The design is printed in up to 8 colors using high-precision rotogravure at +/-0.1mm precision, with food-grade low-migration water-based ink.
- Slitting and die cutting. Printed film is cut to the shape and register that matches the mold cavity. Film thickness runs from 30 micrometres to 100 micrometres, with a maximum printing width of 1200mm.
- Placement in the mold cavity. The cut label is positioned in the open cavity and held by static charge so it does not shift when the mold closes.
- Injection molding and fusion. Molten resin enters the cavity and meets the printed film. The film fuses into the container wall, so the label becomes part of the container rather than an applied surface, which is why peeling does not occur.
- Demolding and quality control. The labeled container leaves the mold with the graphic already finished. YZY applies 100% visual inspection plus random lab testing for FDA and GB compliance across the production run.
How a buyer should run the switch evaluation
- Build the true cost baseline. Collect the label purchase price, adhesive and consumables, labeling labor, line changeover downtime, label-related reject and rework rates, and freight for the separate labeling materials.
- Define the performance envelope. Write down the minimum temperature range, with fill temperature at one end and cold chain at the other, plus chemical exposure, abrasion risk and whether the pack will be squeezed.
- Verify compliance documents before samples. Request the FDA food contact test report, the migration test position under EU 10/2011, and the management system certificates. Compliance issues are cheaper to find on paper than in a production run.
- Run a mold-matched sample trial. Sample performance is only meaningful when the label geometry matches the actual cavity. Confirm adhesion after molding, not simply on a flat printed sheet.
- Compare total cost per 1,000 finished containers. Place the IML quotation next to the baseline from step one. The comparison belongs at container level, not label level.
- Lock the commercial terms. Confirm MOQ, lead time from sample approval, replenishment cycle and technical support before releasing the first production order.
Use Cases: Where IML Fits
| Application | Why IML fits | Specification that carries the load |
|---|---|---|
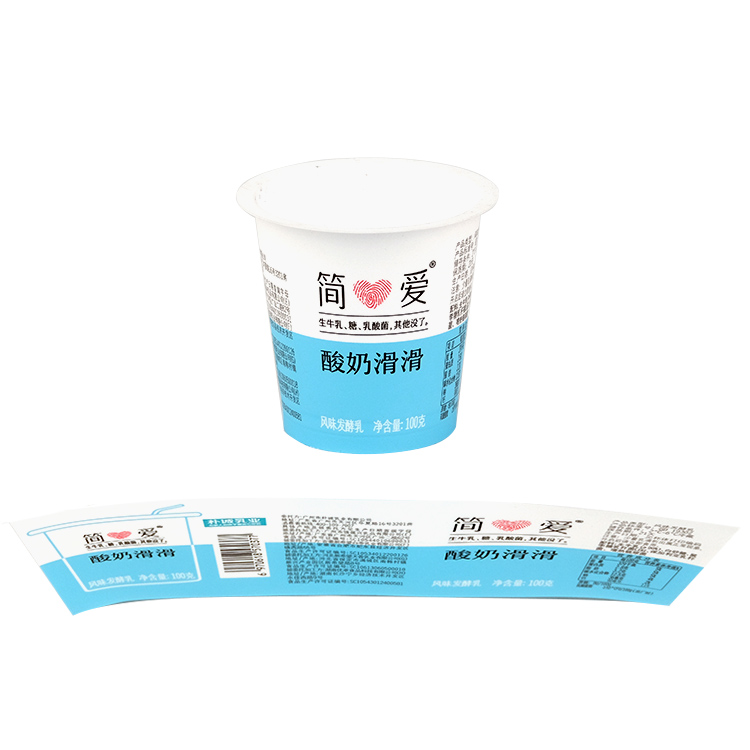
| Yogurt cup | Cold chain and condensation are constant; the label cannot lift or cockle | Adhesion at least 5N, temperature resistance to -20 degrees C, waterproof film construction |
| Bubble tea cup | Fast-moving food service format with high visual standards and repeated handling | 8-color printing at +/-0.1mm, 4H scratch resistance, food-grade low-migration ink |
| Ice cream container | Freezer storage followed by condensation on the shelf | Low-temperature performance to -20 degrees C, no edge lift |
| Paint bucket | Aggressive contents and rough handling in a trade environment | Chemical resistance to weak acids, alkalis and detergents; 4H scratch resistance |
| Lubricant bucket | Oily industrial environment and outdoor storage | PE / PP film compatibility, chemical resistance, impact-resistant fused surface |
| Detergent and shampoo bottle | Daily chemical exposure and squeeze dispensing | Chemical resistance, adhesion at least 5N, glossy or matte finish options |
| Cosmetic container | Premium shelf appearance with premium finishes | Holographic and custom texture finishes, +/-0.1mm print precision |
| Plastic bottle and water bottle | High-speed filling lines and chilled display | Tensile strength at least 20MPa, no warping at production speed |
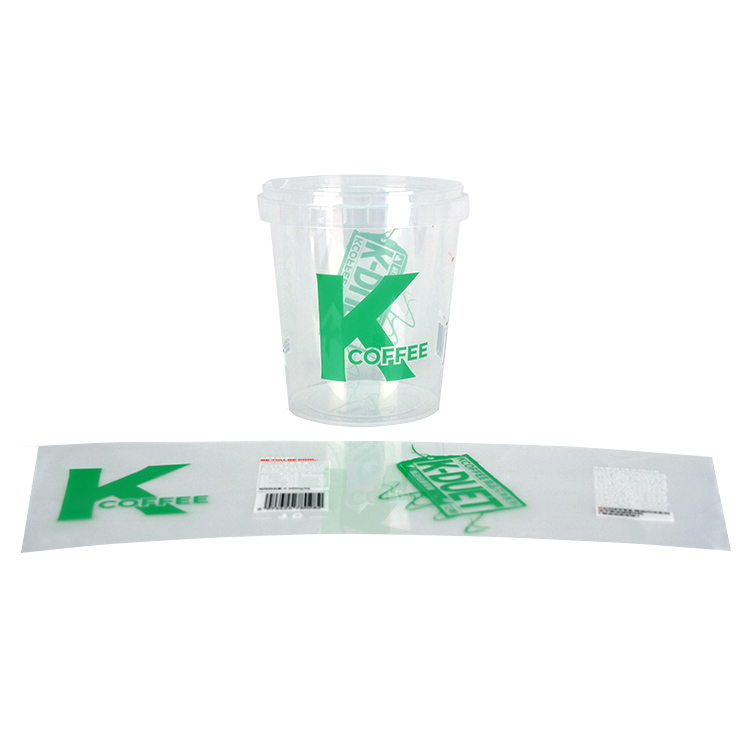
Field evidence supports the table above. YZY has supplied an international food and beverage and dairy brand, operating through injection factories, with custom food-grade IML labels for cold beverage and yogurt cups on a high-volume mass production basis over a one-year engagement. The reported results were zero quality complaints, a 100% on-time delivery rate and 100% compliance, with the delivery footprint spanning markets including DZ, EG, IN, IR, PK, PH, SA, TH, TR, TW, US, UZ, VN and ZA. YZY also reports long-term cooperation with brands such as Starbucks, Nestle and Uni-President.
Comparison Table: IML vs. Traditional Post-Production Labels
| Decision factor | In-mold label (ZY-IML Series) | Traditional post-production label |
|---|---|---|
| When the label is applied | Inside the mold cavity, during injection molding | After the container is molded, on a separate labeling line |
| Label material | PP, PE, PET or multi-layer composite film, 30 to 100 micrometres | Paper or plastic film with an adhesive layer |
| Bond mechanism | Film fuses into the container wall during molding | Adhesive bonds to the finished container surface |
| Peel and edge lift | No peeling during injection molding; adhesion strength at least 5N | Adhesive bond can lift at edges, particularly on curved or squeezable containers |
| Temperature range | -20 degrees C to 120 degrees C, covering cold chain and hot filling | Determined by the adhesive system; hot fill and warm chain require specific adhesive grades |
| Scratch resistance | 4H on the pencil hardness test | Paper face is soft and abrades with handling |
| Chemical resistance | Resistant to weak acids, alkalis and common detergents | Paper and standard adhesives degrade faster under this exposure |
| Production steps | Integrated into the molding cycle; roughly 30% fewer steps than running a separate labeling operation | Adds labeling, handling and inspection as separate steps |
| Lead time | 20% lead time reduction compared with post-production labeling | Baseline |
| Material cost per label | Higher film and ink cost | Lower |
| Labor and rejection cost | No separate labeling labor; label-related rejection and rework are removed with the step | Labeling labor, line downtime and misalignment rejects remain in the cost stack |
| Total cost at volume | Lower once labor, downtime and rejects are counted | Higher at volume |
| Food contact documentation | FDA 21 CFR 177.1520 test report (SGS NGBEC2501946006), EU 10/2011 migration test, BRCGS, ISO22000, QS | Requires separate paper and adhesive food-contact documentation on top of the container file |
| Printing and design | 8-color rotogravure at +/-0.1mm; glossy, matte, orange peel, holographic and custom finishes; maximum printing width 1200mm | Constrained by the adhesive and the paper face |
| Material family | Label film and container share the same polyolefin family (PP / PE) | Paper or film label sits on a plastic container as a separate material |
| Best fit | High-volume food, dairy, ice cream, beverage, paint and detergent packaging | Low-volume runs, non-food items, or packaging with no peeling or condensation risk |
Frequently Asked Questions
Does the ZY-IML Series meet US and EU food contact requirements?
Yes. The ZY-IML Series is certified to the FDA Food Contact Test Report. The certification was issued by SGS under certificate number NGBEC2501946006, based on the FDA 21 CFR 177.1520 standard, with a scope covering food contact packaging materials and an applicable market of the US and North America. For European destinations, the product is tested against the migration requirements of EU Regulation (EU) No 10/2011 for plastic materials intended to come into contact with food. YZY also holds QS, ISO and BRC certifications and applies strict inspection standards from raw materials through to finished products.
What adhesion, temperature and abrasion performance can a buyer specify?
The ZY-IML Series is specified at an adhesion strength of at least 5N, the level at which the label does not peel during injection molding. The operating temperature range is -20 degrees C to 120 degrees C, which covers cold chain distribution and hot filling with the same label construction. Scratch resistance is 4H on the pencil hardness test, tensile strength is at least 20MPa, and the film resists weak acids, alkalis and common detergents. Printing is 8-color high-precision rotogravure at +/-0.1mm precision, and film thickness ranges from 30 micrometres to 100 micrometres.
Is in-mold labeling more expensive than post-production labeling?
Per label, yes. Film and food-grade low-migration ink cost more than a paper label with adhesive. The comparison that matters is total cost per finished container, which includes labeling labor, line downtime, label-related rejects and rework. Because IML is completed inside the molding cycle, it removes roughly 30% of the production steps associated with a separate labeling operation, and eliminating a full processing step is where the material premium is recovered at volume. For very short runs, the balance usually stays with post-production labeling.
How should a buyer validate an in-mold label before mass production?
Ask for samples cut to the actual cavity geometry, and evaluate adhesion after molding rather than on a flat printed sheet. YZY supports OEM / ODM customization of size, shape, color, printing design and material, and confirms a lead time of 15 to 20 days after sample confirmation. Production is supported by 100% visual inspection plus random lab testing for FDA and GB compliance, so the validation stage and the production stage use the same inspection logic.
What lead time, capacity and MOQ should a buyer plan around?
YZY operates a monthly capacity of 350,000,000 pieces, with an MOQ of 2,000 square metres and a lead time of 15 to 20 days after sample confirmation. Export markets cover the EU, US, Middle East and Southeast Asia, and after-sales support includes online technical support, after-sales consultation and quality complaint handling. To start a sample or quotation request, contact the team at yzy@inmoldlabel.net or on WhatsApp at +86 182 6778 1866, and download the in-mold label brochure for the full specification set.
Conclusion
The comparison resolves into a single question: does the label need to survive the container, or does the container need to carry the label? Post-production labeling works when the pack is stable, dry, unremarkable and produced in small batches. In-mold labeling wins when the pack is squeezed, chilled, hot-filled, chemically exposed or handled at high volume, because the label stops being a separate component and becomes part of the container wall.
For a buyer, the practical checklist is short. Confirm the temperature envelope, with -20 degrees C to 120 degrees C covering the majority of food, dairy and beverage formats. Confirm the adhesion specification of at least 5N if peeling has ever been a complaint. Confirm the food contact file, including the FDA 21 CFR 177.1520 test report and the EU 10/2011 migration position. Confirm the 4H scratch resistance if the pack travels on pallets. Then price the change at container level, where the roughly 30% reduction in production steps and the 20% lead time reduction compared with post-production labeling show up as real money.
Next step: sample, quotation or technical review
Send the container geometry, fill temperature and target market, and YZY will match a ZY-IML Series film, finish and label size to the mold. Samples, quotations and compliance documents are available on request.
Email: yzy@inmoldlabel.net | WhatsApp: +86 182 6778 1866 | Website: www.inmoldlabel.net
Download the YZY in-mold label brochure (PDF) for the full film, ink and compliance specification set.
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.